-Some of our Unique Projects-
Measurement & Material Balance
Hightec helped a major US refining company reduce operational gain/loss by $23.6MM, while also increasing earnings by $3.4MM at a major fractionator through overall process optimization. Drawing on 50+ years of combined measurement and material balance experience, the team works directly alongside client operations to flatten out component imbalances. This hands-on approach consistently improves consistency, accuracy, and profitability with minimal capital investment.
Commercial Fundamentals Research
Hightec helped a major US refining company reduce operational gain/loss by $23.6MM, while also increasing earnings by $3.4MM at a major fractionator through overall process optimization. Drawing on 50+ years of combined measurement and material balance experience, the team works directly alongside client operations to flatten out component imbalances. This hands-on approach consistently improves consistency, accuracy, and profitability with minimal capital investment.
100kbp Refinery FEED Study
Hightec delivered Front End Engineering Design (FEED) and Detailed Engineering Design for a new 100,000 bpd refinery in Africa, built around three processing trains sharing a common FCC unit. Construction was phased, starting with a 30,000 bpd train, followed by two additional 35,000 bpd trains, with advanced refining capabilities added to expand specialized product output. The multi-train configuration allowed for staged startup, resilience if one train goes down, and 30 days of feed/product storage buffer with spare capacity for maintenance.
Pipeline Projects
Hightec brings deep regulatory experience, supporting PHMSA and DOT compliance across more than 50,000 miles of onshore and offshore pipelines of various sizes and commodities. The team’s expertise spans the full pipeline lifecycle, from early concept modeling through project execution. A recent project included a complete 6″ discharge gas pipeline replacement for a major Permian Basin operator, completed in record time, under budget, and with a perfect safety track record.
Ethane Blending Project
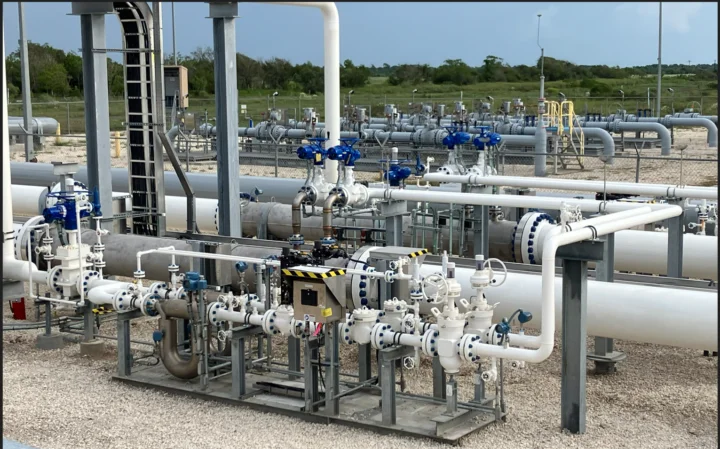
Ethane liquid was being injected into the methane vapor stream at a major fractionation unit, but the original mixer design failed, causing excessively high vibration throughout the pipe and preventing the unit from reaching its target rate of 50,000 barrels/day. Hightec redesigned the system, completing all engineering, fabrication, and construction within just 80 days. The new design started up with zero issues, fully restoring production capability.
Major Gas Processing Plant Fire Rebuild
Hightec was brought in to replace a damaged heat exchanger at a critical 200 MMcf/d processing plant. The team first implemented a bypass solution to get the plant back online quickly, then designed, fabricated, constructed, and commissioned a full replacement heat exchanger. The project was completed before rising summer temperatures could cause a reduction in plant throughput.
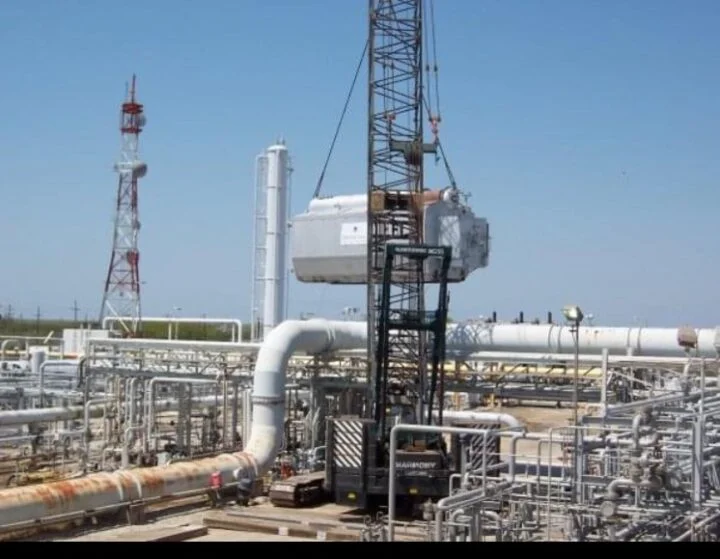
Utility Upgrade Project
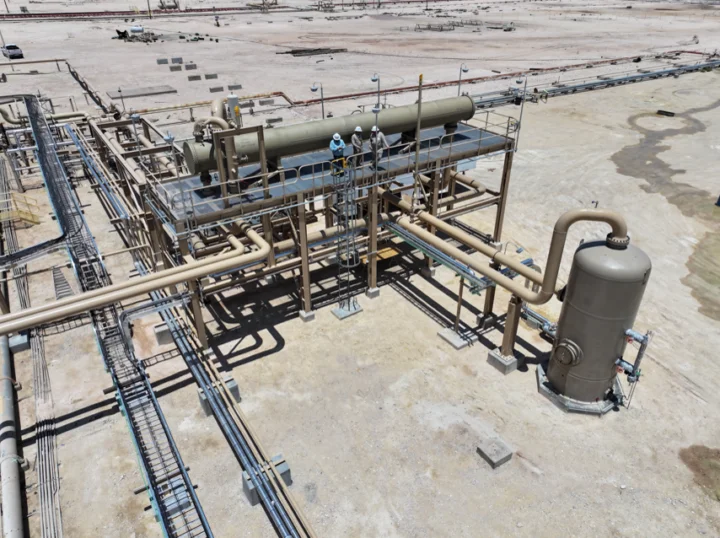
Hightec designed and installed a high-capacity steam boiler system, adding 220,000 kg/hour of steam at 4,200 kPa and 385°C to a 30,000 barrel-per-day refinery. This upgrade also supported an integrated 30 MW power generation unit and a 13 billion cubic meter/year natural gas plant, significantly expanding the facility’s overall utility infrastructure.
Product Loading via Rail and Road
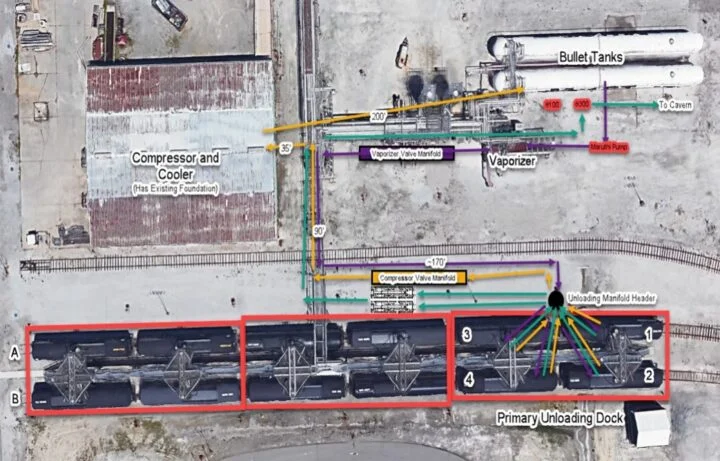
At a product unloading terminal in Marysville, MI, Hightec identified that LPG product was consistently being left behind in the vapor space of every railcar. The team proposed a solution using existing equipment already within the client’s inventory to evacuate the remaining vapor after liquid product retrieval, increasing overall product recovery. The proposal projected a full ROI within one year of installation, along with up to a 10% increase in overall terminal throughput.